Partner Project: Medical Technology Product Marked Inside the Mould
 George Nowill
- 4 minutes read

|
Getting your Trinity Audio player ready...
|
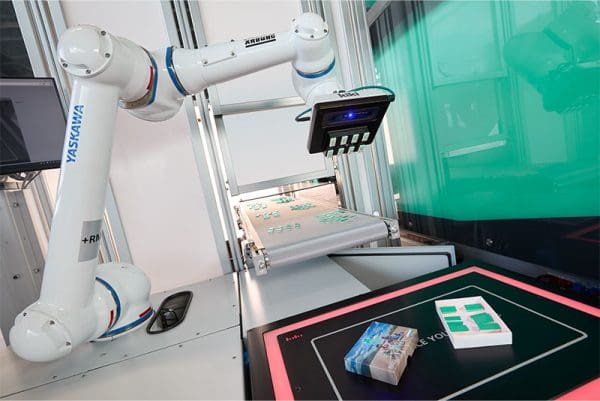
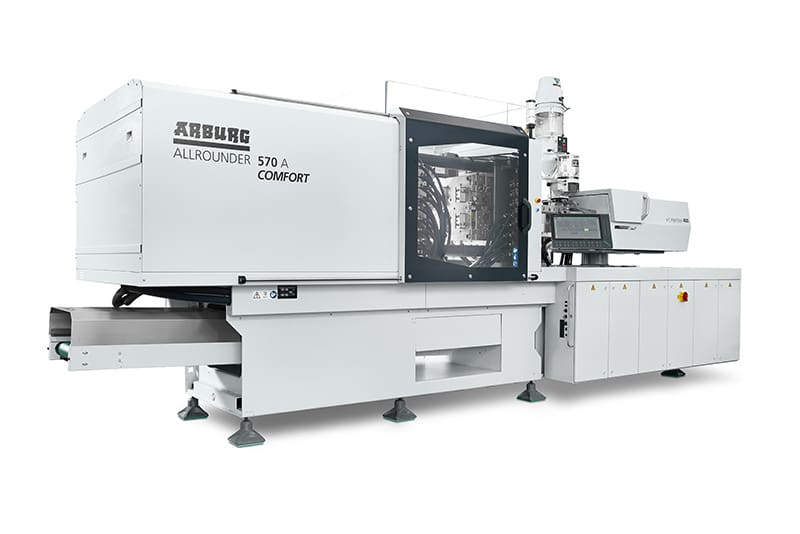
At Fakuma 2026, partners Arburg (injection moulding machine), Kebo (mould) and Matriq (component marking) are demonstrating an innovative marking process for the medical technology sector: an electric Allrounder 570 A injection moulding machine in a cleanroom version, equipped with a 4-cavity mould, is used to produce auto-injector housings as an example.
A dynamic mould insert is fitted with 144 heating elements, each measuring just 0.28 x 0.28 millimetres. Individual Data Matrix codes are applied directly to the component during the injection moulding process. This process is suitable for a wide range of materials, it requires no downstream process steps and it can significantly reduce energy requirement, cycle time and costs.
The exhibit will be presented at the Matriq stand (Hall A4, Stand 4213). At Arburg (Hall A3, Stand 3101), another production cell for the medical technology sector, will be on display; Kebo can be found at Fakuma 2026 in Hall B3, Stand 3313 and Borouge International (material) in Hall A4, Stand 4218.
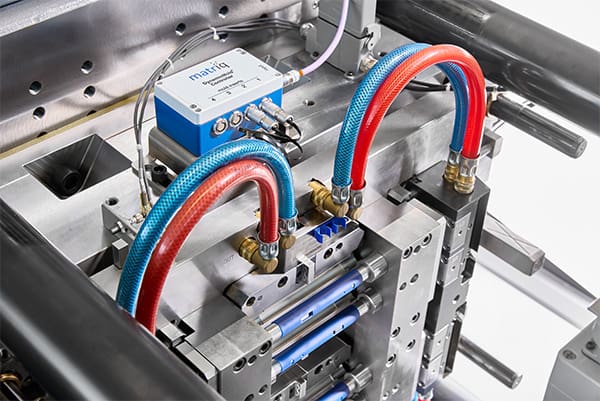
In-line Marking Via Microheaters in the Mould Insert
In a cycle time of around eleven seconds, an electric Allrounder 570 A with a clamping force of 2,000 kN in a cleanroom version will be producing four auto-injector housings at a time. The material used is medical-grade PP (Bormed HG820MO) from Borouge International, coloured blue using a colour batch from the company Color Service. These high-performance machines from the Alldrive series are ideally suited to the fast and precise series production of medical technology products and it satisfies the requirements for production in an ISO Class 7 clean room.
The “aXw Control PressurePilot”, with its biconically optimised pressure regulation within the Gestica control system, ensures consistent mould filling and consistently high part quality.
The 4-cavity mould is based on Kebo’s tried-and-tested “Lift & Strip” concept and is actuated entirely mechanically and synchronously via the machine ejector. It ensures a robust, reproducible process and facilitates a reliable transition from pilot to series production.
The compact, efficient mould concept enables increased productivity. The highlight of the application is a dynamic mould insert integrated into the cavities. This assigns an individual Data Matrix code to each component. The insert features 144 individually controllable microheaters. These are brought up to temperature within milliseconds, thereby creating individual geometric structures. Each microheater measures just 0.28 x 0.28 millimetres and weighs only around 0.0000015 grams (1.5 micrograms) – 20,000 times less than a grain of rice. Subsequent process steps can be omitted. This reduces cycle time, installation area and the costs associated with an additional marking device and robotic system for parts handling.
Medical Devices are 100 Percent Traceable
A central database system communicates with the Gestica machine controller and the Matriq system via an OPC UA interface. An NTP (Network Time Protocol) server synchronises the system time. The part ID and the relevant production and measurement data from the Allrounder, as well as the individual Data Matrix codes, are linked synchronously in the database. The components can then be uniquely identified using a camera system and precisely assigned to the respective production and measurement data. This allows machine data and process parameters – such as date, shot count, injection pressure and material cushion – to be retrieved at any time.
An Efficient Alternative to Lasers and Labels
Matriq AG, a spin-off from the University of Applied Sciences of Eastern Switzerland (OST), develops innovative solutions for the seamless traceability of plastic components. In the application showcased at Fakuma 2026, the Data Matrix code is generated using what Matriq has named its “DM-qode”. Unlike laser marking, this method does not rely on colour contrast but instead on a geometric structure created during the moulding process. This makes the process suitable for a wide range of component colours and materials. For example, it is possible to mark black or transparent plastic parts, as well as those with high filler content.
Applying the code in this way leaves the original material unchanged, i.e. it retains the same chemical structure. Furthermore, this process does not remove any material, nor does it have a thermal impact on the surface of the part. This is particularly relevant for safety-critical or mechanically stressed parts. The process consumes around 20 times less energy than conventional laser systems and requires no additives or consumables such as RFID tags or in-mould labels. It operates without producing any particulate and it is compatible with cleanroom environments. Currently, this technology can be used for mould temperatures of up to 100 degrees Celsius. A cooling solution for the mould insert is already under development.

ARBURG
01926 457000
Email
Website